Colourinn Industries – Textile & Dyes Auxiliaries Manufacturer & Exporter

Blog

  1. Home
  2. /
  3. Blog

Top 10 Types of Textile Chemicals for Global Buyers

Textile chemicals sit at the quiet center of modern fabric production. They help cotton absorb dyes, polyester resist wrinkles, and technical fabrics repel water. Yet every chemical choice leaves a practical question: what happens after finishing, washing, or disposal?

The 2024 Textile Exchange Materials Market Report estimated global fiber production at about 132 million tonnes in 2023. It projects nearly 160 million tonnes by 2030. More fabric means more chemical decisions. The United Nations Environment Programme also reports that textiles contribute significantly to global greenhouse-gas emissions and water pollution. Exact estimates vary. That uncertainty deserves attention.

This guide examines ten major types of textile chemicals, including pretreatment agents, dyes, enzymes, softeners, coatings, and water-treatment chemicals. It focuses on function, purchasing risks, and measurable performance. A bright sample is not enough. Buyers should also examine restricted-substance screening, wastewater data, biodegradability claims, and supplier traceability.

Michael Braungart, a chemist and co-founder of the Cradle to Cradle Products Innovation Institute, states, “Waste equals food.” That principle challenges buyers to consider chemical recovery and safer material cycles, not only production speed.

No single chemical is automatically sustainable. Dosage, process temperature, worker protection, wastewater treatment, and end-of-life conditions all matter. This is where many purchasing decisions become less certain. Supplier certificates can help, but they should never replace independent verification. A careful buyer asks harder questions. Sometimes, the honest answer is still incomplete.
Top 10 Types of Textile Chemicals for Global Buyers

Textile Chemicals: Definition, Scope, and Role in Textile Manufacturing

Textile Chemicals: Definition, Scope, and Role in Textile Manufacturing

Textile chemicals are substances used to clean, color, protect, soften, or finish fibers and fabrics. Their scope covers the entire production route, from fiber preparation to garment finishing. Common categories include pretreatment agents, wetting agents, detergents, chelating agents, bleaching stabilizers, dyes, pigments, leveling agents, softeners, and water-repellent finishes. Each type changes how fabric looks, feels, performs, or processes.

In practical mill assessments, chemical selection begins with fiber type, fabric construction, water quality, and process temperature. Cotton may require alkaline preparation, while synthetic fibers often need different dispersing and leveling support. A softener can improve hand feel, but excessive use may reduce absorbency or create uneven shades. Small errors matter. Operators should check technical data sheets, safety data sheets, batch records, and supplier test results before production. Laboratory trials should measure shade, shrinkage, pH, color fastness, and fabric strength.

Textile chemicals also influence wastewater quality and workplace safety. Responsible buyers should request information on restricted substances, biodegradability claims, storage conditions, and treatment requirements. Local regulations may differ, so one approval cannot cover every destination market. That assumption is risky. Reliable sourcing includes sample testing, traceable documentation, and periodic factory checks. Even experienced teams can miss a compatibility problem when formulas change. A controlled trial often reveals more than a confident specification.

How Textile Chemicals Are Classified by Function and Production Stage

Top 10 Types of Textile Chemicals for Global Buyers

How Textile Chemicals Are Classified by Function and Production Stage

Textile chemicals are easier to evaluate when buyers connect function with production stage. During fiber preparation, antistatic agents and spin finishes control friction and reduce fiber breakage. Lubricants help synthetic filaments move smoothly through guides and rollers. In spinning, sizing agents strengthen yarns and limit abrasion during weaving. Common sizing materials include starch derivatives, acrylic polymers, and modified cellulose. Their performance depends on yarn type, machine speed, and later removal requirements.

Pretreatment chemicals prepare fabric for color and finishing. Surfactants improve wetting, while scouring agents remove oils, waxes, and loose impurities. Chelating agents control metal ions in hard water. Bleaching auxiliaries support even whiteness and protect fiber strength. Desizing enzymes remove sizing residues with lower processing temperatures. During dyeing, dyes, leveling agents, dispersants, and fixing agents control shade uniformity. Printing uses thickeners, binders, and defoamers. Finishing may involve softeners, water repellents, crease-control agents, or antimicrobial treatments.

For global purchasing, classification should include compliance and process data. In mill audits, I have seen a small pH difference change the final shade noticeably. Request technical data sheets, safety data sheets, recommended dosage ranges, and wastewater guidance. Check restricted-substance requirements in every destination market. A product may perform well in one mill but fail with different water hardness or machinery. No classification system is perfect. Buyers should test chemicals on actual fabric, record bath conditions, and review results after washing, drying, and storage.

Top 10 Types of Textile Chemicals for Global Buyers

Textile chemicals are commonly classified by their primary function and the production stage where they are applied. The chart uses 1 to indicate a typical application stage and 0 to indicate that the chemical is not normally used at that stage.

Pretreatment chemicals prepare fibers for coloration, coloration chemicals support dyeing and printing, and finishing chemicals modify the final textile properties such as softness, water repellency, and surface performance.

Ten Major Types of Textile Chemicals for Global Buyers

Ten Major Types of Textile Chemicals for Global Buyers

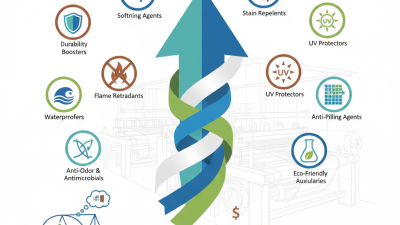
Textile buyers usually evaluate ten major chemical types: pretreatment agents, wetting agents, scouring agents, bleaching agents, dyes, pigments, fixing agents, softeners, finishing agents, and auxiliaries. Each type serves a different production stage. Pretreatment chemicals remove oils and sizing residues before dyeing. Wetting agents help water penetrate dense fibers. Scouring agents clean cotton, blends, and technical fabrics. Bleaching agents improve brightness, but require careful control of temperature and concentration.

Dyes create color inside fibers, while pigments remain closer to the fabric surface and need suitable binders. Fixing agents improve color fastness after dyeing. Softeners change handle, drape, and surface comfort. Finishing agents may add wrinkle resistance, water repellency, flame resistance, or antimicrobial performance where regulations permit. Other auxiliaries support foam control, pH adjustment, leveling, and bath stability. Small chemical changes can affect shade accuracy.

Global buyers should request safety data sheets, technical data, restricted-substance declarations, and batch information. Independent testing is useful. It can reveal problems hidden in a supplier’s sample. I have seen a fabric pass a color test but fail after repeated washing because the process was not reproduced accurately. That weakness matters. Buyers should compare performance, dosage, wastewater requirements, storage conditions, and worker protection measures, not only price. Some formulations also need reformulation for different fibers, climates, or local treatment systems. A reliable supplier explains limitations clearly, even when the answer is inconvenient.

Top 10 Types of Textile Chemicals for Global Buyers - Ten Major Types of Textile Chemicals for Global Buyers

No. Textile Chemical Type Primary Function Common Chemical Forms Typical Process Stage Common Fiber or Product Uses Key Buying and Technical Considerations
1 Dyes and Colorants Provide durable color and visual consistency to textile fibers, yarns, and finished fabrics. Reactive dyes, disperse dyes, acid dyes, direct dyes, vat dyes, sulfur dyes, and pigment colorants. Dyeing or printing. Reactive dyes are widely used for cotton and other cellulosic fibers; disperse dyes are mainly used for polyester; acid dyes are commonly used for wool, silk, and polyamide. Evaluate fiber compatibility, shade reproducibility, fixation rate, colorfastness, restricted-substance compliance, wastewater load, and suitability for the intended process.
2 Sizing Agents Increase yarn strength, reduce hairiness, and improve abrasion resistance during weaving. Modified starch, polyvinyl alcohol, carboxymethyl cellulose, acrylic polymers, and polyester-based sizing polymers. Warp sizing before weaving. Primarily used for cotton, polyester-cotton blends, and other woven yarns. Consider sizing efficiency, viscosity, compatibility with the loom, ease of desizing, biodegradability, and impact on fabric hand and absorbency.
3 Wetting, Scouring, and Detergent Auxiliaries Remove oils, waxes, dirt, spinning lubricants, and processing residues while improving water penetration. Nonionic or anionic surfactants, emulsifiers, detergents, penetrants, and low-foam cleaning agents. Desizing, scouring, washing, and preparation. Used across cotton, linen, viscose, polyester, polyamide, and blended fabrics. Check low-foam performance, cleaning power, bath stability, compatibility with enzymes and dyes, wastewater biodegradability, and performance at the target temperature.
4 Bleaching Agents and Stabilizers Improve whiteness and remove natural coloration before dyeing or printing. Hydrogen peroxide, sodium chlorite, sodium hydrosulfite, peroxide stabilizers, and bleaching activators. Bleaching and optical preparation. Hydrogen peroxide is widely used for cotton and other cellulosic fibers; reducing bleaches are used in selected synthetic-fiber processes. Assess whiteness level, fiber-strength retention, metal-ion control, decomposition safety, pH requirements, effluent impact, and compatibility with downstream dyes.
5 Dyeing Auxiliaries Improve dye dispersion, wetting, migration, exhaustion, fixation, and process uniformity. Dispersing agents, leveling agents, sequestering agents, antifoams, pH buffers, carriers, and electrolyte-management auxiliaries. Dye bath preparation and dyeing. Used for cellulosic, synthetic, protein, and blended-fiber dyeing systems. Review compatibility with the dye class, liquor ratio, temperature profile, foam control, shade evenness, staining risk, and removal from the final fabric.
6 Fixing Agents Improve color fixation and wet fastness after dyeing, especially for cellulosic fabrics. Polyamine-based, cationic, polymeric, and formaldehyde-free fixing agents. After-dyeing treatment and finishing. Frequently applied to cotton, viscose, linen, and their blends dyed with reactive or direct dyes. Consider wet-rubbing and washing fastness, shade change, effect on lightfastness, formaldehyde content, handle, re-dyeability, and restricted-substance requirements.
7 Softening Agents Improve fabric softness, smoothness, drape, sewability, and surface comfort. Silicone emulsions, cationic softeners, nonionic softeners, fatty-acid derivatives, and polyethylene-based softeners. Final finishing, padding, exhaustion, or garment washing. Used on cotton, viscose, polyester, polyamide, wool, denim, towels, knits, and blended fabrics. Select according to desired hand feel, hydrophilicity, yellowing resistance, absorbency, shade impact, shear stability, rewetting behavior, and silicone-management needs.
8 Water- and Oil-Repellent Finishes Reduce wetting and liquid penetration while preserving fabric appearance and comfort as required. Fluorine-free hydrocarbon, silicone, dendrimer, paraffin, and polymer dispersion technologies. Functional finishing and coating. Outdoor apparel, workwear, upholstery, home textiles, tents, and technical fabrics. Compare spray rating, hydrostatic resistance, oil repellency where required, durability after laundering, breathability, curing conditions, hand feel, and environmental profile.
9 Flame-Retardant Chemicals Reduce flame spread, heat release, or afterglow to help fabrics meet specified fire-performance requirements. Phosphorus-based, nitrogen-phosphorus, mineral, organohalogen, and intumescent systems, depending on the application. Back-coating, padding, exhaustion, or polymer finishing. Protective clothing, upholstery, curtains, transport textiles, institutional textiles, and selected home-furnishing fabrics. Verify the applicable fire standard, durability after washing, smoke and gas characteristics, fabric-strength impact, hand feel, curing requirements, and chemical-regulatory status.
10 Textile Enzymes Provide selective biological treatment for desizing, biopolishing, denim effects, and surface cleaning. Amylase, cellulase, pectinase, laccase, catalase, lipase, and protease preparations. Desizing, scouring, biopolishing, denim washing, and peroxide removal. Cellulase is commonly used on cotton and cellulosic fabrics; amylase is used for starch-size removal; catalase helps decompose residual hydrogen peroxide. Control pH, temperature, treatment time, enzyme concentration, water hardness, and deactivation conditions; assess fabric-strength loss, reproducibility, storage stability, and worker-safety requirements.

Performance, Safety, and Compliance Factors in Chemical Selection

Global buyers choosing textile chemicals need more than shade, softness, or price. The ten common categories include wetting agents, detergents, enzymes, dyes, fixatives, softeners, water repellents, flame retardants, antimicrobial finishes, and process auxiliaries. Each choice affects worker exposure, wastewater, fabric durability, and product claims. UNEP’s Sustainability and Circularity in the Textile Value Chain report estimates textiles generate 2–8% of global greenhouse gas emissions. Low-temperature processing matters. The European Environment Agency reported approximately 270 kilograms of textile-related greenhouse gas emissions per EU resident in 2020.

Compliance should begin with full chemical disclosure, batch traceability, and supplier test records. Buyers should screen formulations against the ZDHC Manufacturing Restricted Substances List and verify wastewater performance through independent laboratory testing. Check pH, chemical oxygen demand, color, heavy metals, and persistent substances. A safety data sheet alone is not enough. It may describe hazards, but not real mill conditions. Practical audits often find poor ventilation, unlabeled containers, or inconsistent dosing. These details can undermine an otherwise careful purchasing program. A perfect scorecard is unrealistic. Still, buyers can compare biodegradability, worker protection, recycled-content compatibility, and finishing durability. The EU Strategy for Sustainable and Circular Textiles also emphasizes durability and safer chemical use, linking performance with longer product life. Claims should be evidence-based, not simply printed on a certificate.

How Global Buyers Evaluate and Source Textile Chemical Suppliers

Top 10 Types of Textile Chemicals for Global Buyers

Global buyers evaluate textile chemical suppliers beyond product lists. Common categories include pretreatment agents, dyes, fixing agents, softeners, wetting agents, dispersants, leveling agents, coating chemicals, flame retardants, and finishing auxiliaries. Each type affects fabric appearance, hand feel, color fastness, production speed, or wastewater load.

A reliable supplier should provide a current SDS, technical data sheet, COA, batch traceability, and clear storage instructions. Buyers should also confirm product consistency through laboratory samples and controlled mill trials. Ask about application temperature, dosage, pH range, and compatibility with cotton, polyester, or blended fabrics. Compliance documentation matters, especially for restricted substances and destination-market requirements. A low price may look attractive. It can hide unstable quality.

Communication is another practical test. Suppliers should answer technical questions clearly and disclose lead times, minimum order quantities, packaging details, and transport conditions. In my experience, delayed replies often predict slower problem-solving after purchase. Still, supplier evaluation is not perfect. A successful sample cannot guarantee every future batch.

Tips: Request two or three production samples, not one. Compare whiteness, shade, softness, and reprocessing results. Keep written trial records. Review them with your dyeing technician before signing a long-term agreement.